Renex Pharma was established to use the very best in product development and manufacturing processes with high-quality control parameters to supply innovative medicines and much-needed healthcare products at fair prices to consumers across the world.
Building on our core values of focus, collaboration and excellent product development, we have achieved continuous growth since our establishment.
"Life's not just about staying alive... it's about being well!"
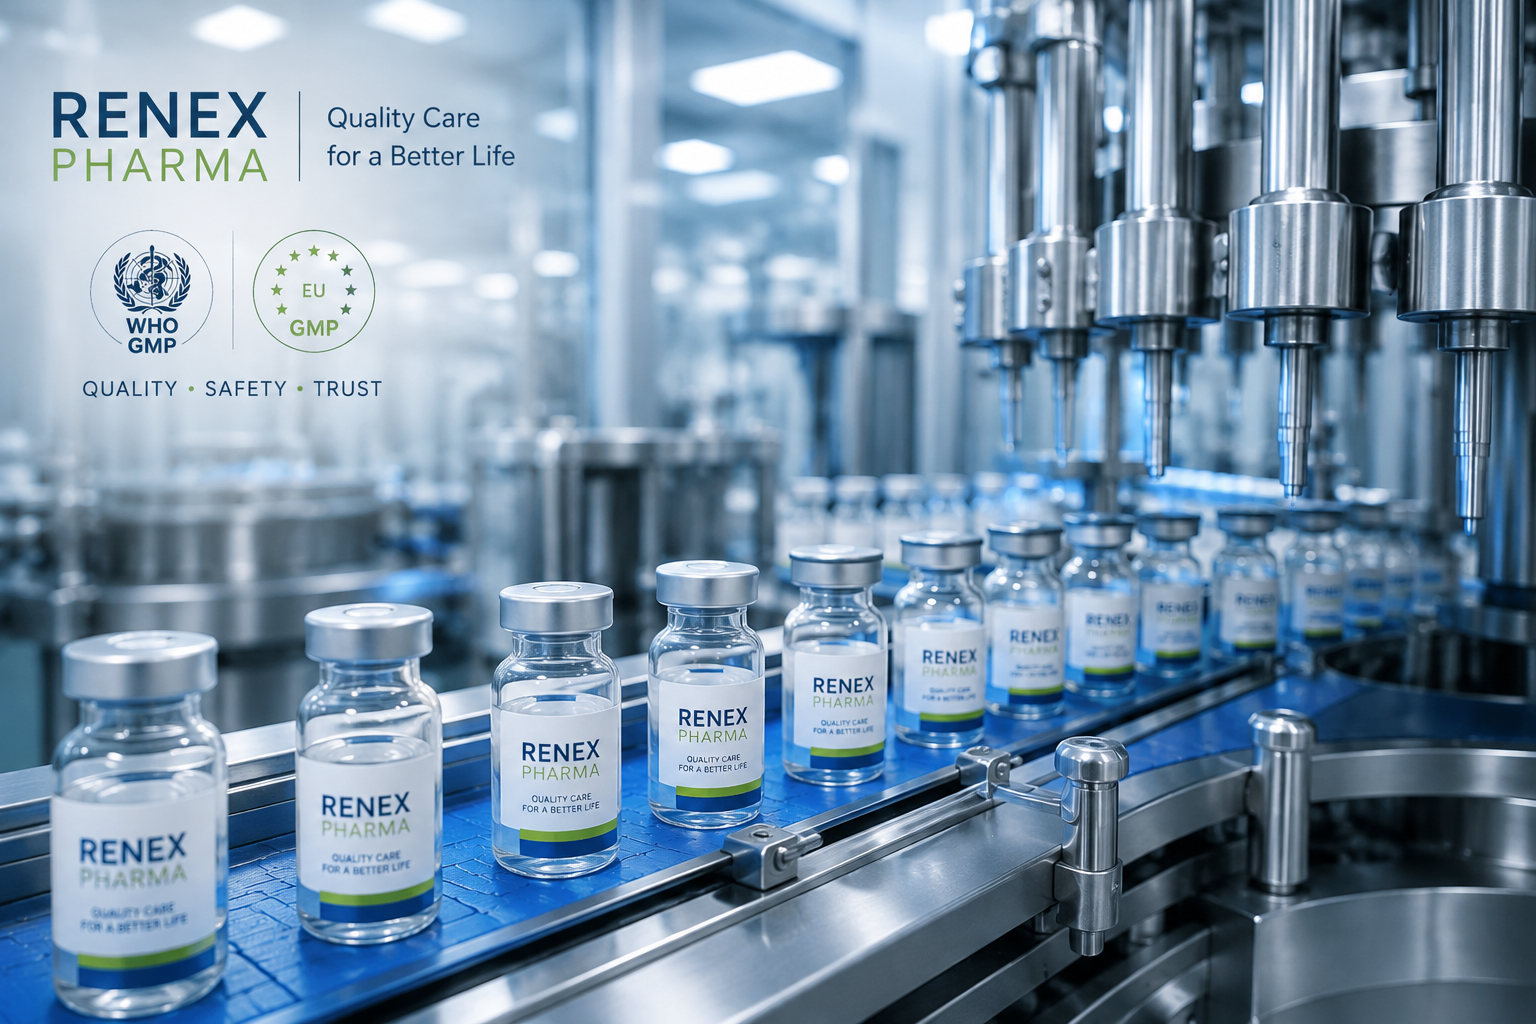
We have a WHO-GMP manufacturing pharma factory located in India. According to international regulatory guidelines, the EUGMP-approved plant in India is built and approved by WHO, EUGMP, MOH of different countries, and other regulatory agencies.
It is well-equipped with a hi-tech HVAC system in our WHO-GMP pharmaceutical and nutraceuticals manufacturing plant ensuring low humidity and an international standard of cleanliness.
An ample amount of space is provided for packing materials, raw materials, manufacturing area, in-process QC, finished goods storage, QC lab, and an effluent treatment plant that serves as an incredible platform for GMP pharmaceutical manufacturing of high-quality medicines at affordable rates.
Every equipment, raw material and packing material used in the manufacturing process are the best in their class and as required by cGMP.
Our EUGMP pharma manufacturing plant is capable of manufacturing solid orals, liquids, syrups, dry syrups, dry powder syrups, external preparations, gels, creams, ointments and other formulations.
With a qualified, trained and dedicated workforce, we maintain adherence to established quality standards to assure the safety and efficacy of our products.
We have a world-class Regulatory Affairs team with vast experience in global regulatory management. Our team is highly responsible for registering in MOH of different countries and defending Renex Pharma's products filing to various regulatory bodies globally.
The Regulatory Team makes and implements registration strategies to ensure that the Company's products comply with international regulations.
Quality par excellence and delivering seamlessly is our hallmark. As a leading WHO-GMP Certified third-party manufacturer, our company's quality supervision is demonstrated at all phases of the product life cycle.
Our quality evaluation starts with careful documentation. This guarantees compliance with good laboratory practices and consequently, the integrity of the data produced.
Quality supervision is continued for distribution, production, and conclusion for the shelf life of the product.
All major stages of the manufacturing process are validated to ascertain that every GMP pharmaceutical product is manufactured to the highest accepted standards.
Our Quality Control department works consistently with precise analytical methods and is equipped with sophisticated modern instruments.
We strive for 100% customer satisfaction through continuous improvements in systems and processes, delivering consistent quality and meeting international standards.
Our customers, our products and our employees are the foundation of our organization. Our mission is to make all our customers grow profitably with time due to their collaborative association with us.
Our vision is to achieve worldwide recognition as the most reliable pharma export business partner that provides customers with superior quality GMP pharmacy at highly affordable prices and consistently follows up with reliable service.